
Product Specifications
- Brand
- Friedrich Vollmer Feinmessgerätebau GmbH
- Part Number
- AGC
- Type
- Automatic Gauge Control System
- Application
- Cold Rolling Mills (Steel, Aluminium, Copper, Precious Metals)
- Gauge Technologies
- Contact, Laser, X-Ray/Isotope
- Contact Accuracy
- ±0.5 µm
- Laser Scan Rate
- 80 kHz (Spot: 0.1 mm)
- Control Modes
- Feedback, Feed-Forward, Mass Flow, Direct Roll Gap, Roll Force
- Communication
- PROFINET, PROFIBUS, TCP/IP
Product Description
The Friedrich Vollmer AGC system provides closed-loop thickness regulation for cold rolling mills, integrating thickness measurement sensors with high-speed servo-hydraulic screwdown control (HAGC). As the only manufacturer offering the complete spectrum of gauge technologies — contact, laser, and X-ray — from a single source, Vollmer can match the measurement principle to each mill stand position and material type without compromise.
What AGC control strategies does the system support?
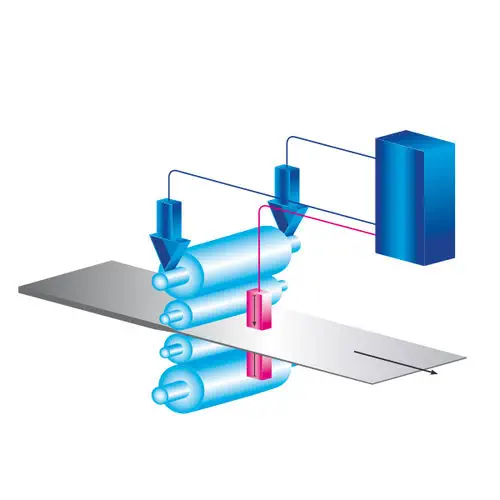
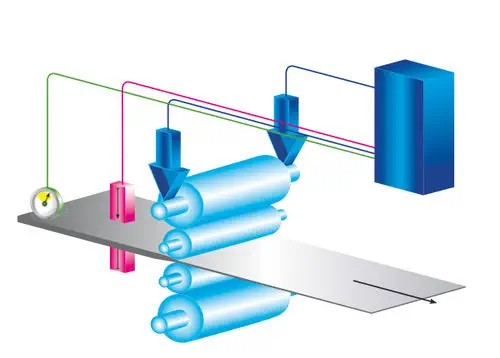
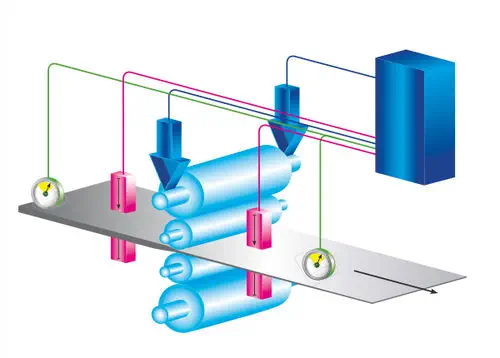
The AGC system implements five core strategies that can be combined for different pass types and mill configurations. Feedback (monitor) control measures exit thickness and adjusts the roll gap to correct downstream deviations — the universal fallback. Feed-forward control measures incoming strip thickness before the bite and pre-positions the gap before the deviation enters, eliminating transport delay. Mass flow control uses the constant-volume principle — entry speed × entry thickness = exit speed × exit thickness — for fast response without exit-side gauge delay. Direct roll gap control places position sensors at the work-roll necks on both drive and operator sides, measuring inside the force flow for the shortest possible signal path and millisecond-level response. Roll force control uses the gaugemeter principle to infer thickness from mill stretch characteristics.
How do the three gauge technologies compare?
| Technology | Accuracy | Range | Best For |
|---|---|---|---|
| Contact (VBM/VBK/VBF) | ±0.5 µm | 0.005–24 mm | Alloy-independent absolute measurement, foil to plate |
| Laser (VTLG) | ±1 µm/mm | 0.003–20 mm | Non-contact in-stand, cross-profile scanning, emulsion environments |
| X-Ray/Isotope | ±0.1% of nominal | Application-dependent | Coated strip, multi-layer, tandem mills, galvanizing lines |
The laser gauge uses a 405 nm blue laser with tri-lens focusing optics and a 0.1 mm spot diameter, self-calibrating with four certified gauge blocks before every pass. It can distinguish between the strip surface and oil or emulsion film via software-based temperature compensation models. Contact gauges use diamond-tipped transducers touching both sides of the strip simultaneously, delivering alloy-independent absolute measurement — over 2,500 units installed since 1963.
What makes direct roll gap control the fastest AGC signal?
By placing position sensors directly at the work-roll necks — both drive side and operator side — direct roll gap control measures inside the force flow rather than outside the mill housing. This eliminates the elasticity, bearing play, and housing deformation that delay conventional screwdown position feedback. The result is millisecond-level gap correction during transients such as head/tail of coil, speed changes, and weld passes. Fewer off-gauge passes mean better material yield and reduced scrap.
Vollmer AGC Automatic Gauge Control System for Cold Rolling Mill Thickness Regulation
Product Specifications
- Brand
- Friedrich Vollmer Feinmessgerätebau GmbH
- Part Number
- AGC
- Type
- Automatic Gauge Control System
- Application
- Cold Rolling Mills (Steel, Aluminium, Copper, Precious Metals)
- Gauge Technologies
- Contact, Laser, X-Ray/Isotope
- Contact Accuracy
- ±0.5 µm
- Laser Scan Rate
- 80 kHz (Spot: 0.1 mm)
- Control Modes
- Feedback, Feed-Forward, Mass Flow, Direct Roll Gap, Roll Force
- Communication
- PROFINET, PROFIBUS, TCP/IP